

4-Roll Plate Bending Machines
EBR METAL 4-roll plate bending machines are hydraulic. The plate is held between the top and bottom rolls and moved by the rotating rolls, while the two side rolls pre-bend its ends and roll it. The range has three models, 4V HMK, 4V HMR and 4V HM, which differ in roll movement, driven rolls and working length.
Types of 4-Roll Plate Bending Machines
4-roll plate bending machines differ in how the bottom and side rolls move and which rolls are driven. In the EBR METAL range, two models use pyramidal-linear roll movement and one uses orbital movement.
Pyramidal-Linear Roll Movement (4V HMK, 4V HMR)
On the 4V HMK and the 4V HMR, hydraulic pistons move the bottom roll and the two side rolls in straight lines.
Orbital Roll Movement (4V HM)
On the 4V HM, hydraulic pistons move the bottom roll and the side rolls on an orbital path.
Driven Rolls
The 4V HMK has three driven rolls: hydromotors and planetary gearboxes drive the top roll and both side rolls. The 4V HMR drives its top roll with an electric motor and planetary gearbox, and its bottom roll through a cardan joint system. The 4V HM uses a hydromotor and planetary gearbox on the top roll and a gear and cardan system on the bottom roll.
Swipe to view →
| Feature | 4V HMK | 4V HMR | 4V HM |
|---|---|---|---|
| Roll movement | Pyramidal-linear | Pyramidal-linear | Orbital |
| Driven rolls | Top roll and both side rolls | Top and bottom rolls | Top and bottom rolls |
| Top roll drive | Hydromotor and planetary gearbox | Electric motor and planetary gearbox | Hydromotor and planetary gearbox |
| Working length | 2,050–6,100 mm | 650–4,100 mm | 1,550–4,100 mm |
| Control options | NC or CNC | NC | NC or CNC |
Explore Our Plate Rolls Portfolio
Browse the three models below.
4-Roll Hydraulic Plate
Bending Machine
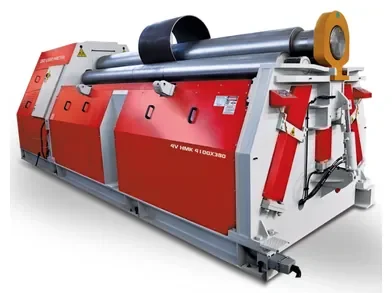
4V HMK (4-Roll)
Three driven rolls and pyramidal-linear roll movement, for working lengths from 2,050 to 6,100 mm. NC or CNC control is optional.
Hydraulic Plate Roller
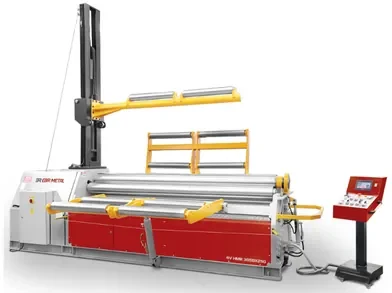
4V HMR (4-Roll)
Pyramidal-linear roll movement with a motor-driven top roll and a cardan-driven bottom roll; 3 digital readouts for roll positioning. Working lengths run from 650 to 4,100 mm, and NC control is optional.
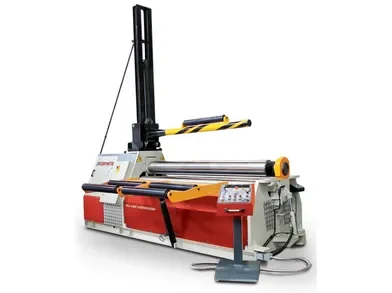
Hydraulic Plate Rolls
4V HM (4-Roll)
Orbital roll movement; hydromotor and planetary gearbox on the top roll. Working lengths from 1,550 to 4,100 mm, with NC or CNC control as options.
Why Choose 4-Roll Plate Bending Machines?
On a 4-roll machine, the plate is held between the top and bottom rolls and moved by the rotating rolls. The side rolls are used both for pre-bending and for rolling. Usually both plate ends are pre-bent in turn without taking the plate out of the machine, and 4-roll machines generally leave shorter flat ends than 3-roll machines.
Pre-Bending and Flat Ends
The capacity tables in the EBR technical catalogue give separate figures for work with and without pre-bending. Without pre-bending, a flat section can remain at each end of the plate, depending on the diameter.
Circular, Oval and Conical Parts
Depending on the model, its equipment and its capacity, the 4-roll machines roll full circles, elliptical (oval) shapes and parts with different diameters. Cones are rolled with the conical bending device.
Selection Basics
Match the working length, the maximum plate thickness and the minimum and maximum diameter to your parts. Tell us whether the capacity must include pre-bending. For large diameters or thin walls, side and top supports may be needed.
Applications & Materials
Material, thickness and how sensitive the surface is all shape the configuration we propose.
Typical Applications
All three models are suited to this work; the right model depends on the thickness, the working length and the diameter.
- Tank and silo shells
- Pressure-vessel parts
- Machinery bodies
Materials and Capacity
Capacities are stated for a reference carbon-steel grade. For stainless steel, aluminium and other grades, we check the capacity for your actual material (see Capacity and Material Grade on the Plate Rolling Machines page).
Controls and Large-Diameter Support
NC control is available on all three models, and CNC control on the 4V HMK and the 4V HM. The NC control has a teach mode: the operator bends a part while the controller records each step, and the saved program repeats the same sequence on the next part.
Each model keeps its rolls parallel with a balancing system: hydraulic on the 4V HMR and the 4V HM, and hydraulic or electronic on the 4V HMK depending on roll size. For large diameters, all three can be fitted with hydraulic lateral side supports and an overhead crane.
4-Roll Machines Built to Order
Besides the three standard models, EBR METAL builds 4-roll machines to order, including custom machines for conical work and for bending pre-corrugated sheet, and automatic or semi-automatic systems that take sheet from a feeding table, roll it and send the finished part to a stack. Where the job needs it, the rolls, the machine configuration and the operating mechanism are adapted. There are no standard capacities or model codes for this work.
Choose the Right 4-Roll Plate Bending Machine
Send us the material type and grade, the thinnest and thickest plate you will roll, the maximum working length, the minimum inside diameter and whether the capacity must include pre-bending. For cones, add the cone angle and both diameters.
Frequently Asked Questions
What’s the advantage of 4-roll vs 3-roll?
Usually both plate ends are pre-bent in turn without taking the plate out of the machine, and the flat ends are generally shorter than on a 3-roll machine. The right choice between 3-roll and 4-roll depends on the part geometry, the pre-bending you need, the capacity and your production conditions. See Plate Rolling Machines.
Does pre-bending change the capacity?
Yes. The EBR technical catalogue lists capacity with pre-bending and without it separately.
How do I size the machine?
Match the working length, the maximum plate thickness and the minimum and maximum diameter to your parts, and state whether the capacity must include pre-bending. Supports may be needed for large diameters.
Can I roll cones?
Yes, with a conical bending device. Send us the cone angle, both diameters, the thickness and the length so we can check the machine and configuration.
Do I need NC or CNC?
NC control is available on all three models and has a teach mode that records the bending steps of a part and repeats them. CNC control is available on the 4V HMK and the 4V HM.
Which model suits the longest plates?
The 4V HMK, with working lengths up to 6,100 mm. The 4V HMR covers 650 to 4,100 mm and the 4V HM 1,550 to 4,100 mm.