

Project Overview
In 2022, EBR METAL completed a deep drawing hydraulic press project for a boiler systems manufacturer in Australia. The customer produces boiler heads, upper and lower boiler covers, the body sections between them, and project-based pressure tanks. Until this project, the boiler head / dish end components were sourced from outside suppliers.
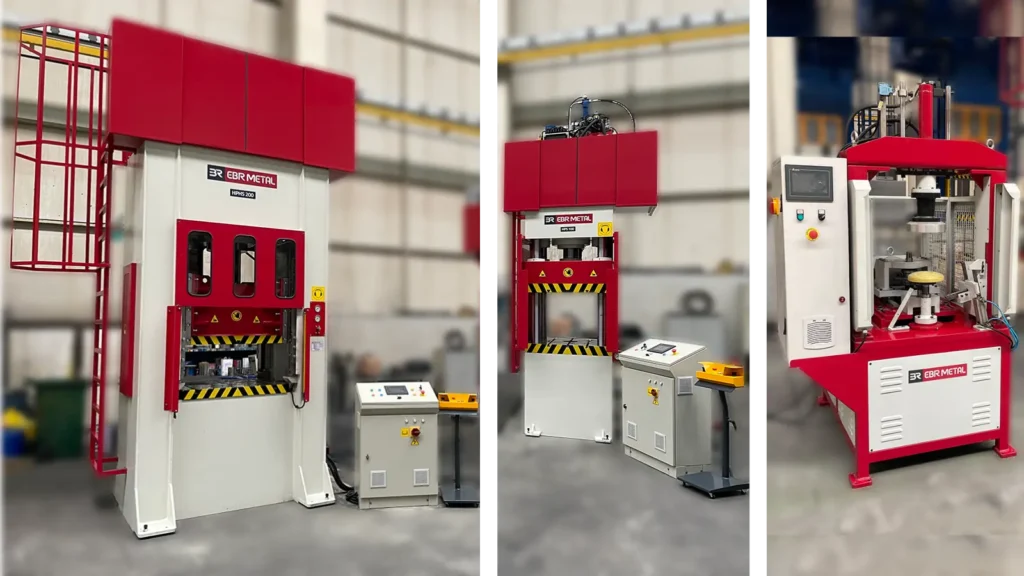
EBR METAL supplied a turnkey, project-specific production setup — two hydraulic presses, a hydraulic trimming and beading machine, and a complete set of forming and punching dies — that brought dish end production in-house. The system starts from a prepared stainless steel blank sheet and produces a formed, punched, trimmed and deburred boiler head, ready for the welding stage.
All machinery is CE certified and built with Rexroth hydraulic components and Siemens / Schneider electrical components. The machines were fitted with standard safety equipment such as light curtains and safety guards, and the electrical system was arranged for the customer’s 400/440V supply.
Scope of Supply
- 1 x HPHS 200/100 Double Action Hydraulic Press
- 1 x HPS 100 Column Type Press
- 1 x Hydraulic Trimming and Flanging Machine
- 3 x Forming Dies for Stainless Steel Dish Heads
- 3 x Punching Dies for Dish Heads
- 1 x Forming Die for Round Feet (Base Ring)
Together, these machines and dies formed a project-specific setup for stainless steel dish head forming and boiler head production — from the first deep drawing operation to punching, trimming and deburring before welding.
Project Photos
Machinery and Tooling Delivered
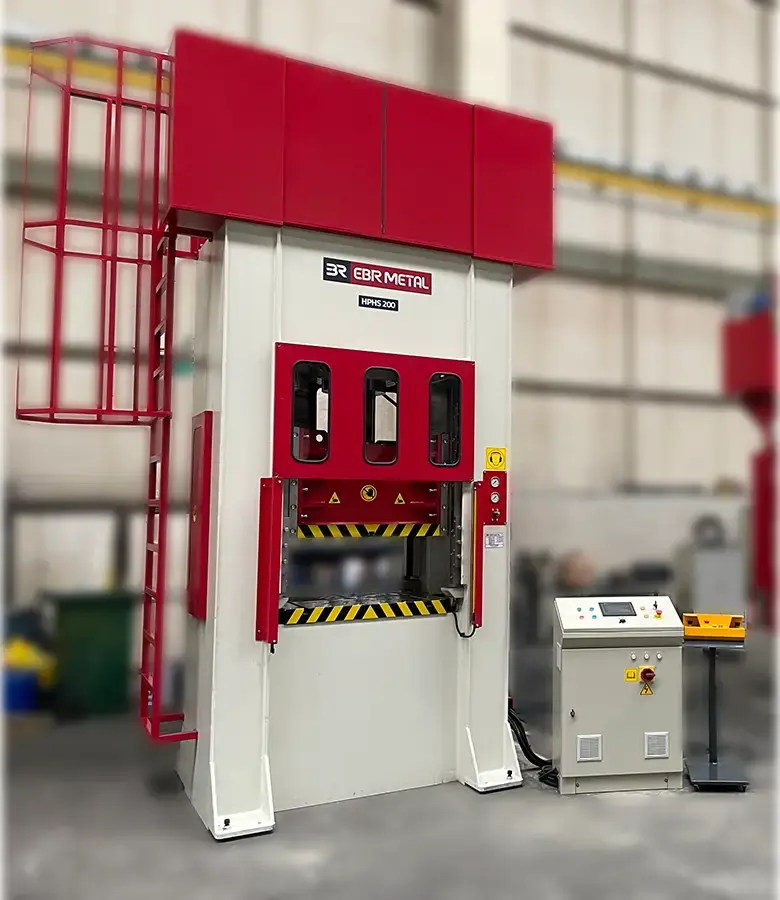
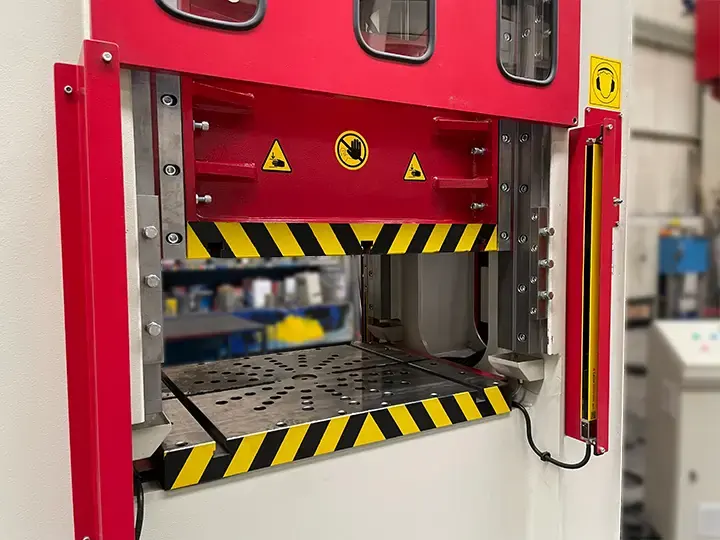
H Type Hydraulic Deep Drawing Press – 200/100 Ton
Application: Deep drawing, stainless steel forming
Technical Details:
- Nominal Pressure: 200/100 Tons
- Slide Stroke: 600 mm
- Table Size: 800 x 1000 mm
- Slide Size: 800 x 1000 mm
- Daylight: 700 mm
- Cylinder Type: Triple action synchronized hydraulic cylinders
- Frame Structure: Monoblock – H Type – 8 Guided
The HPHS 200/100 is a double action hydraulic press built for stainless steel deep drawing. The 200/100 ton configuration separates drawing force from blank-holding force, which keeps material flow under control as the blank is drawn into its domed form. The monoblock H-type frame with 8-point slide guiding holds alignment under off-center loads during repetitive dish head forming.
Forming stainless sheet in 2–3 mm thickness is sensitive to blank-holder pressure and die geometry. Drawing on its experience with domed forming dies, EBR METAL completed the trial runs on this project without wrinkling problems on the required diameters.
Column Type Hydraulic Press – 100 Ton
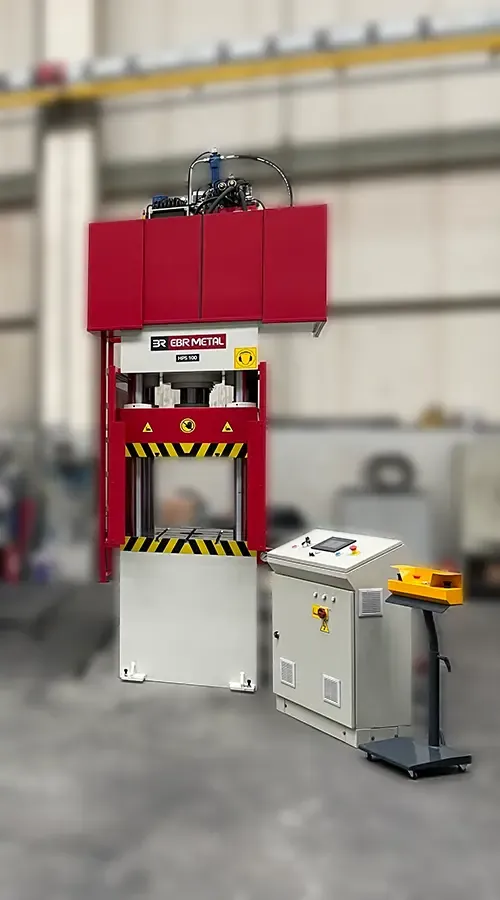
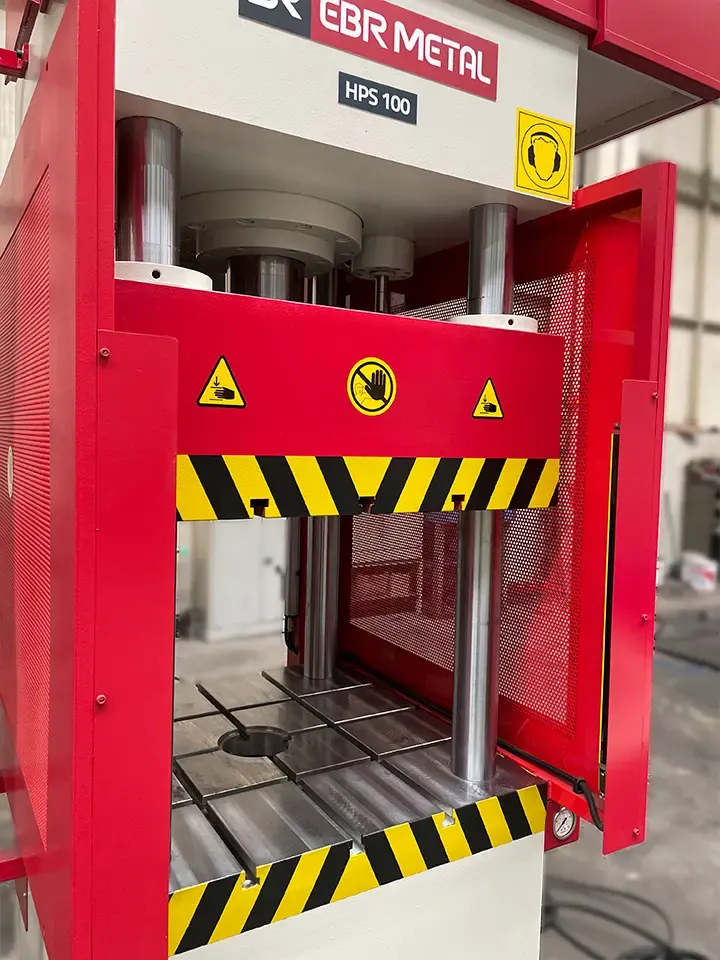
The HPS 100 four column hydraulic press handles the punching stage of this project. Hole configurations vary by part — some boiler heads need 2 holes, while others need 3 holes with different diameters — and four column guiding keeps the slide parallel during punching.
The same press also forms the round feet / base ring sections that allow the finished boiler to stand vertically.
Application: Punching, pressing, flattening and base ring forming processes
Technical Details:
- Nominal Pressure: 100 Tons
- Slide Stroke: 400 mm
- Table Size: 600 x 600 mm
- Slide Size: 600 x 600 mm
- Daylight: 500 mm
- Cylinder Type: Top-mounted, down stroke single cylinder
- Frame Structure: Four column guide
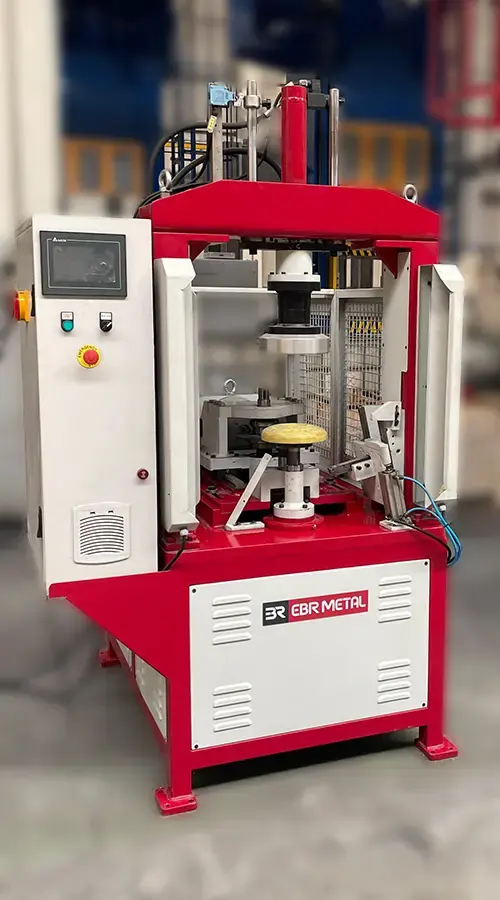
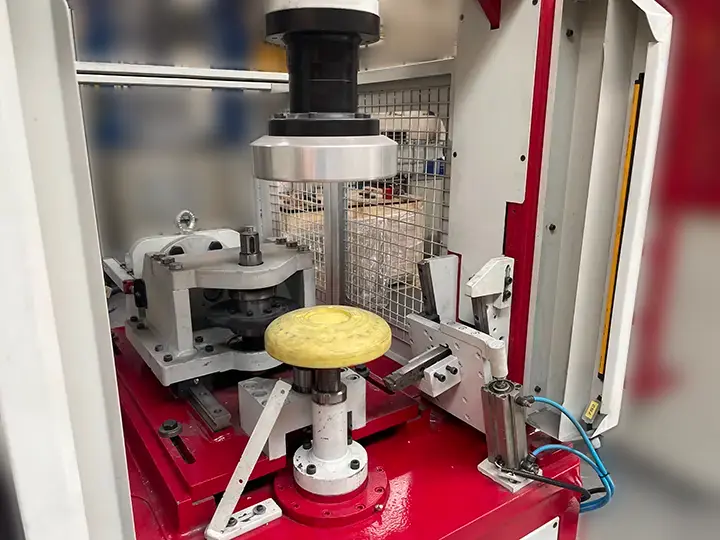
Hydraulic Trimming & Beading Machine
- Hydraulic clamping
- Max. cutting & beading diameter: 500 mm
- Max. cutting & beading thickness: 4 mm stainless steel
- Special alloy steel blades for cutting stainless steel
- Deburring unit with carbide cutting inserts
After forming and punching, dish heads move to the hydraulic trimming and flanging machine for edge cutting, beading and burr removal.
Cutting leaves burrs on the edge, and burrs are a real problem at the next stage: in automatic welding they can cause poor weld quality, holes in the weld seam, or sections that cannot be welded properly. To solve this, EBR METAL added a deburring unit to the machine. The unit uses carbide cutting inserts — the same insert type used in CNC lathes and machining centers — to remove burrs after trimming and leave a weld-ready edge.
Die Set: 9 Product Variations with 3 Punching Dies
The tooling side of the project carried as much engineering work as the presses.
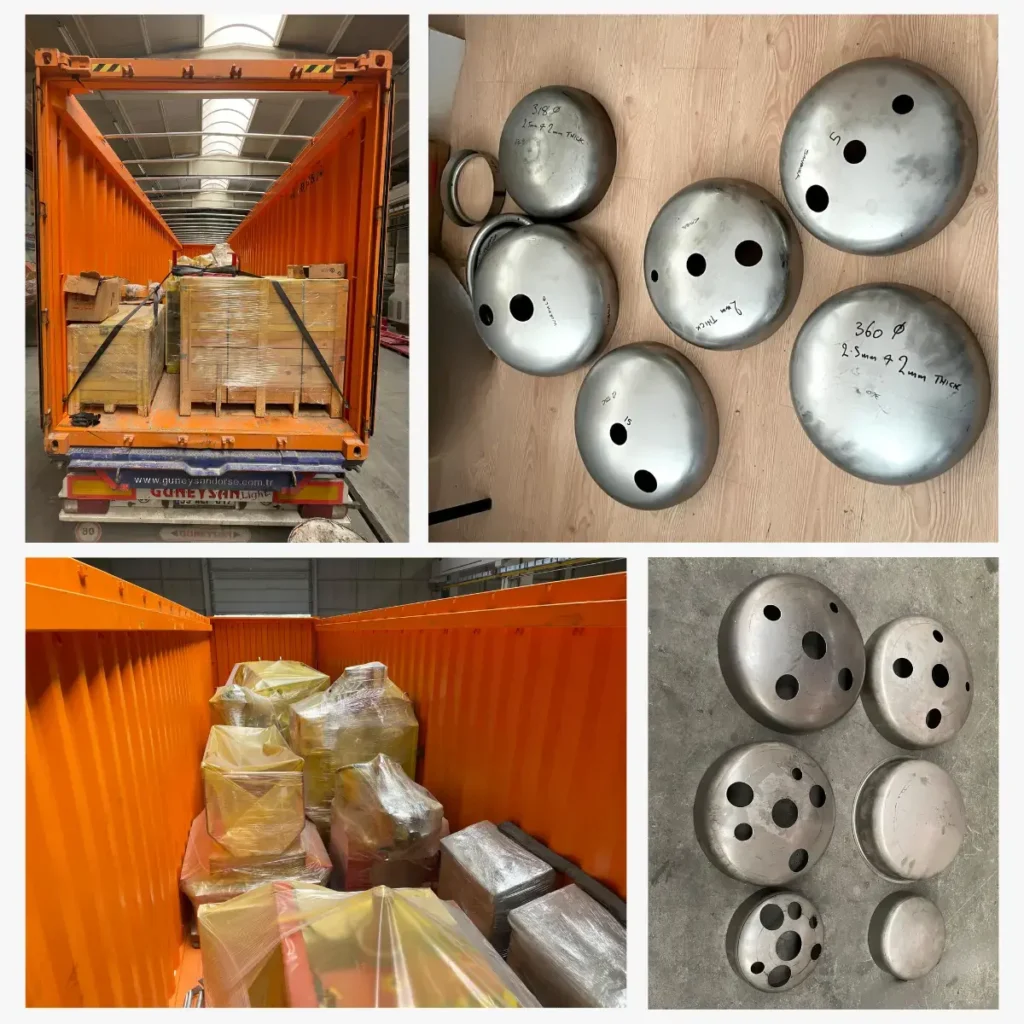
Three forming dies were manufactured for the customer’s three dish head diameters: 360 mm, 318 mm and 216 mm. Three punching dies were built for the same diameters. Hole counts and hole diameters change from product to product, so a straightforward approach would have required up to 9 separate punching dies.
Instead, EBR METAL designed the punch sections to be activated or deactivated depending on the product. With this arrangement, the 3 punching dies cover around 9 product variations across the three diameters — lower tooling cost and shorter production preparation time for the customer.
The same logic was applied to the base ring tooling: a single forming die produces two different sizes of boiler feet.
Working in 2–3 mm stainless steel set the technical bar for this die set. Die materials, cutting angles, punching angles and forming parameters were all critical for trouble-free operation over the die’s working life, so the design and drawing phase took longer than usual, and machining time increased because the tooling had to be precise and error-free before trials began.
Testing and Customer Approval
Before shipment, every machine was tested electrically and mechanically, then run together with the dies through multiple trial production runs. The working process of all three machines was recorded in photos and video, and the trial footage was shared with the customer. Shipment proceeded after the customer approved the trial results.
Shipment to Australia
The machines were shipped partially disassembled and loaded into one 40-foot open-top container as 12 packages, with the dies packed in wooden crates and the remaining machine parts prepared for ocean transport. Lashing was completed by a specialist lashing company, and — due to COVID-period Australian import requirements — fumigation was carried out by an authorized, certified fumigation company before shipment. Every loading stage was photographed and recorded on video.
What the Project Changed for the Customer
Before this project, the customer was buying boiler head / dish end components from outside suppliers. With this setup, production moved in-house: less dependency on external suppliers, higher production capacity, and the freedom to switch between diameters and hole configurations as orders require.
The result is faster and more economical supply of pressure vessel components — with part quality under the customer’s own control.
Related Hydraulic Press Solutions
EBR METAL manufactures hydraulic presses for deep drawing, forming and punching work, along with project-specific forming dies. If your production involves dish heads, boiler heads, tank components or other drawn stainless parts, these pages cover the related machinery:
Start Your Forming Project
Planning a dish head, boiler head or pressure vessel forming project? Send us your part drawings, material grade and expected production volume. Our engineering team reviews the application first — including whether a multi-variation die approach like this project can reduce your tooling cost — then proposes a press and tooling configuration that matches it.
Learn about EBR METAL
Discuss a Similar Forming Project
Explore Hydraulic Press Solutions
EBR METAL designs hydraulic press and tooling setups for deep drawing, punching, trimming and forming applications.